
6 Best Welding Consumables For Remote Repair Kits For Field Use
Equip your field gear with these 6 best welding consumables for remote repair kits. Optimize your on-site performance and reliability. Read our expert guide today.
A snapped control arm or a cracked frame rail miles from civilization turns an epic trek into a mechanical nightmare. Carrying a focused selection of welding consumables transforms a vehicle from a potential liability into a self-sufficient basecamp. Selecting the right rods and wire for the trail requires prioritizing versatility and performance in compromised conditions.

|

|

|
|
$17.99
|
$21.79
|
$71.61
|
Disclosure: As an Amazon Associate, this site earns from qualifying purchases. Thank you!
Hobart 6011 Stick Electrode: Best For Dirty Metal
When mud, rust, or trail debris are present, Hobart 6011 rods are the gold standard for field repair. This electrode features an aggressive arc that punches through surface contaminants, minimizing the need for extensive metal prep when time is short. Its deep penetration and ability to operate in any position make it indispensable for tight, awkward underside welds.
The 6011 is not designed for aesthetic, smooth-looking beads, so expect a rougher finish that prioritizes function over form. However, for a structural gusset that needs to hold a vehicle together to get back to the pavement, it is unmatched. Keep a small pack of these in the rig for the grimiest, most urgent structural fixes.
Lincoln Electric 7018 Rod: Best Structural Repair
The Lincoln Electric 7018 rod is the professional’s choice for high-strength, low-hydrogen structural repairs. These rods produce a smooth, professional-grade bead with high impact toughness, making them ideal for critical load-bearing components like suspension mounts or trailer hitches. They are significantly less prone to cracking than faster-burning rods, providing peace of mind on technical terrain.
Note that 7018 rods require a clean, dry surface to perform effectively, as they are moisture-sensitive. If the repair area is heavily rusted or coated in thick mud, a quick grind is essential before striking an arc. These belong in every kit for long-term repairs where structural integrity is the absolute priority.
Blue Demon E71T-11 Flux Core Wire: Best For Spools
For those running a portable wire-feed welder, Blue Demon E71T-11 flux core wire offers excellent versatility without the need for cumbersome gas bottles. This self-shielding wire creates its own gas coverage, allowing for reliable welds even in windy, open-field conditions. It handles mill scale and minor surface impurities surprisingly well for a wire process.
This wire is an ideal choice for multi-pass welds where speed and ease of setup are required. Because it is flux-cored, the slag cleanup is straightforward, which is beneficial when working under a vehicle on uneven ground. Ensure the spool is protected from moisture during storage to prevent wire oxidation.
Forney 6013 Welding Rods: Best For Thin Sheet Metal
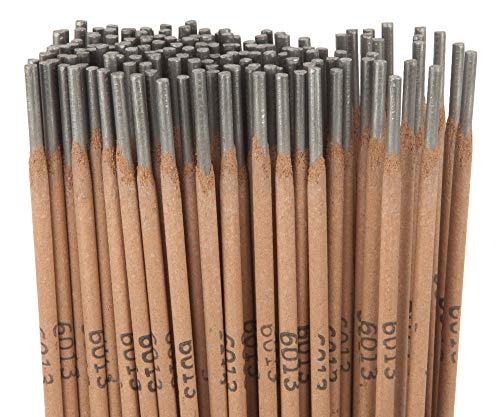
Forney 6013 electrodes excel when trail repairs involve thin-gauge steel, such as body panels, oil pans, or brackets. Their soft, stable arc makes them much easier to control than faster-burning rods, significantly reducing the risk of blowing a hole through thinner material. This predictability is a major advantage when attempting a delicate fix in a stressful, remote setting.
While these rods are not intended for high-stress structural joints, they are superior for light-duty sheet metal work. Their ability to provide a clean, visually appealing weld makes them the go-to for body-focused repairs. If the repair involves thinner metal, having these in the kit prevents the common pitfall of over-welding and damaging the surrounding structure.
Hobart 7014 Stick Electrode: High Deposition Rates
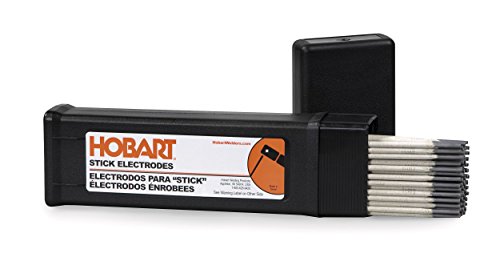
The Hobart 7014 is designed for efficiency, offering a higher deposition rate that fills gaps quickly. This is particularly useful when the damaged metal has significant fitment gaps or missing chunks that require substantial filler material. The rods run smoothly and are quite forgiving, making them accessible even for those who weld only occasionally.
These electrodes are generally intended for use on clean or slightly cleaned steel surfaces. While not as aggressive as the 6011, they offer a perfect balance between ease of use and weld strength. They are a reliable middle-ground choice for general-purpose repairs that fall somewhere between structural necessities and cosmetic fixes.
Lincoln Electric Fleetweld 6010: Deep Penetration

The Lincoln Electric Fleetweld 6010 is the preferred choice for situations requiring maximum penetration into thick base metal. Its ability to “dig” into the workpiece makes it perfect for heavy-wall steel, such as thick-walled bumper tubing or heavy recovery points. It provides a tight, controlled arc that works well even when fit-up is less than ideal.
Operating 6010 rods demands a steady hand and some familiarity with electrode manipulation techniques. Because they are designed for deep penetration, they are aggressive and can easily cut through thin material if the settings are not dialed in correctly. Keep these as the “heavy artillery” in the welding kit for the most challenging structural steel repairs.
How To Store Welding Rods Dry In Your Overland Rig
Moisture is the enemy of high-quality welds, particularly for low-hydrogen electrodes like the 7018. Utilize dedicated, airtight plastic rod canisters with O-ring seals to prevent atmospheric moisture from compromising the flux coating. These canisters are rugged enough to withstand the vibrations of corrugated fire roads and river crossings.
Beyond the canister, consider placing a few desiccant packs inside each tube to absorb any trapped humidity. Keep these canisters inside the vehicle’s cabin rather than mounted externally where they are exposed to rain or splashing. Maintaining dry rods is the single most effective way to ensure a successful weld when a breakdown occurs.
Powering Your Welder With Dual Vehicle Batteries
Running a portable welder off a vehicle electrical system requires a high-output alternator and a robust dual-battery setup. Ensure the primary and auxiliary batteries are connected via a high-amp isolator to protect the starting battery from being drained during the welding process. Always keep the engine at a high idle while welding to provide the necessary current without stalling the vehicle or burning out components.
Monitor the battery voltage closely during use, as excessive current draw can lead to sudden power loss in critical vehicle systems. Using heavy-gauge jumper cables or welding leads is mandatory to minimize voltage drop and heat buildup between the battery and the welding machine. When used correctly, a dual-battery system provides a powerful, mobile power source for any trail repair.
Fire Safety And Prevention For Remote Trail Welding
Welding in the backcountry presents an immediate fire risk from molten sparks and slag. Always clear a three-foot radius of all dry grass, leaves, and flammable trail debris before striking an arc. Carry a high-capacity fire extinguisher specifically rated for electrical and chemical fires, and keep a shovel or water jug within arm’s reach of the repair site.
Never weld near fuel lines, fuel tanks, or spilled oil without implementing a physical heat shield, such as a welding blanket or scrap sheet metal. The sparks generated during field repairs can easily travel behind body panels or into hidden crevices, leading to smoldering fires that are difficult to extinguish. Prioritizing fire prevention is as critical as the weld itself to ensure the repair doesn’t lead to a total vehicle loss.
Prepping Broken Metal Components For Trail Repair
A clean joint is the foundation of a durable trail-side weld. Use an angle grinder with a flap disc or a wire wheel to strip paint, rust, and scale back at least an inch from the repair area. If power tools are unavailable, a quality hand file or a stiff wire brush is necessary to ensure the arc can bond to bare, conductive metal.
Proper fit-up is just as important as cleanliness; take the time to hammer or realign broken parts so the gap is minimal. Welding a large gap is significantly harder than welding a tight, well-fitted joint, especially in sub-optimal conditions. Rushing the prep phase often leads to failed repairs, so invest the extra ten minutes to get the metal surface ready for a solid bond.
Equipping your rig with these essential welding consumables turns the uncertainty of remote travel into a manageable endeavor. By understanding the specific strengths of each rod and wire, you gain the ability to tackle mechanical failures with confidence and precision. Pack your kit wisely, prioritize safety above all else, and you will find that even the most remote trails become significantly more accessible.
Frequently Asked Questions (FAQs)
What are the best welding consumables for remote repair kits in field operations?
Remote repair kits for field operations typically perform best with versatile consumables like E6011 cellulosic electrodes, E7018-H4R moisture-resistant rods, self-shielded flux-cored wire, and ER70S-6 TIG cut lengths. These consumables tolerate surface contaminants such as rust and paint while operating without bulky external shielding gas bottles. Carrying small 5-pound waterproof tubes of stick rods and a 2-pound spool of gasless wire covers carbon steel, pipeline, and structural fixes in remote environments.
What does an all-position welding rod do in mobile field repair?
All-position welding rods allow mobile technicians to weld joints overhead, vertically, horizontally, or flat without moving heavy, damaged equipment. Electrodes with an AWS designation ending in 1, such as E6010 or E7018, utilize specialized flux coatings that freeze molten slag quickly to support the weld puddle. This feature proves critical in field repair where disassembling structural machinery or flipping tractor implements is physically impossible.
How do I store low-hydrogen welding consumables in a field repair kit without an oven?
Low-hydrogen welding consumables can be stored effectively in the field using hermetically sealed, O-ring gasketed rod canisters paired with reusable silica gel desiccant packs. Field operators should only open factory-sealed vacuum cans when ready to weld, immediately transferring remaining electrodes into sealed PVC or aluminum storage tubes. For high-critical structural welds, consume E7018 rods within four to nine hours of opening, or substitute moisture-resistant E7018-H4R formulations that withstand ambient humidity longer.
How do you prep rusted steel in the field before using repair electrodes?
Steel preparation in the field requires removing thick scale, grease, and loose rust down to sound metal using a coarse wire wheel, flap disc, or cold chisel. Solvents like acetone clean oil deposits that cause hydrogen cracking, while grinding creates a clean landing for the ground clamp to prevent arc blow. If deep grinding is impractical in the field, choosing a deep-penetrating E6010 or E6011 rod burns directly through light surface rust and mill scale reliably.
Which is better for emergency field repairs on farm equipment, E6010 or E7018?
Emergency field repairs on farm equipment usually favor E6010 rods because their cellulose coating penetrates through rust, dirt, and paint without requiring a perfectly clean joint. E7018 produces stronger, more crack-resistant welds with higher impact toughness, but requires pristine metal and strict moisture control to avoid porosity. A common field practice uses E6010 for the dirty root pass to bridge poor fit-up gaps, followed by E7018 fill passes to maximize structural strength.
How many pounds of welding electrodes should you pack in a mobile repair kit?
Mobile repair kits generally require 10 to 20 pounds of welding electrodes split across several diameters and alloys to handle standard emergency service calls. A balanced kit often contains 5 pounds of 1/8-inch E6011, 5 pounds of 1/8-inch E7018, and 2 to 3 pounds of specialized 309L stainless rods for joining dissimilar metals. Packing more than 25 pounds adds unnecessary vehicle weight and risks consumable spoilage from extended exposure to field moisture and temperature fluctuations.
Why is flux-cored wire creating worm tracks or porosity during outdoor field welding?
Worm tracks and porosity in gasless flux-cored field welding are usually caused by excessive arc voltage, incorrect wire stickout, or trapped moisture on the steel. Running self-shielded wire (such as E71T-11) with an electrode extension shorter than 1/2 inch or longer than 3/4 inch disrupts flux gas generation. Lowering machine voltage by 1 to 2 volts, drying the joint with a propane torch, and confirming the welder is set to direct current electrode negative (DCEN) normally resolves the issue.
Is it safe to use cellulose welding rods on high-strength structural steel in the field?
Cellulose welding rods are generally unsafe for high-strength structural steels because their high hydrogen moisture content creates a significant risk of underbead cracking. Steels with yield strengths above 50,000 psi require low-hydrogen consumables, such as E7018 or E8018, along with appropriate preheating between 200°F and 400°F. Reserve cellulosic rods like E6010 and E6011 strictly for low-carbon mild steel, non-critical pipe joints, and emergency tack welds where high ductility and low hydrogen are not mandatory.