
6 Best Welding Electrodes For Low-Amperage Field Use
Find the 6 best welding electrodes for low-amperage field use. Read our expert guide to choose the right rods for your portable welding projects today.
A roadside breakdown in the backcountry or a fractured rack on a remote expedition can turn a dream trip into a logistical nightmare. Having the capability to perform emergency field repairs with a portable welder ensures that a broken piece of gear does not signal the end of the adventure. Selecting the correct electrode for these low-amperage, field-based situations is the difference between a structural fix and a wasted rod.

|
|

|
|
$14.40
|
$107.48
|
$89.99
|
Disclosure: As an Amazon Associate, this site earns from qualifying purchases. Thank you!
Forney 30301 E6013: Best for Thin Metals
When addressing thin-walled tubing on mountain bike racks or lightweight stove components, high-heat rods often blow right through the base metal. The Forney 30301 E6013 offers a softer arc that is specifically engineered for these delicate, low-amperage applications. Its ease of striking and stable arc make it the primary choice for those with limited welding hours.
Because this rod produces less spatter and creates a shallow, manageable penetration, it prevents the structural warping that ruins thin sheet metal. It remains a forgiving electrode that compensates for shaky hands in cold or windy field conditions. If the repair involves light-gauge steel, this is the rod to have in the kit.
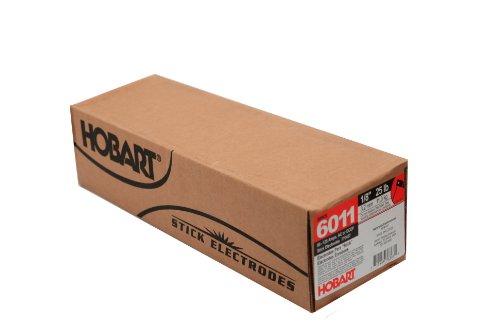
Hobart 6011 Stick: Best for Dirty Field Use
Field repairs rarely happen in a clean shop environment, and metal is almost always coated in rust, grease, or trail grime. The Hobart 6011 is a fast-freezing, deep-penetrating electrode designed to burn through contaminants that would choke other rods. It acts as an aggressive cleaner, ensuring a bond even when conditions are less than ideal.
While it does produce significant spatter, the trade-off is superior fusion in non-optimal circumstances. It performs exceptionally well on thick, structural components like trailer hitches or heavy-duty roof rack supports. For critical, load-bearing repairs where the metal surface cannot be perfectly prepped, the Hobart 6011 is the most reliable option.
Lincoln Fleetweld 180: Best Penetration
Deep penetration is required when welding through thick, rusted steel plates or repairing heavy frame components where the gap is inconsistent. The Lincoln Fleetweld 180 provides the necessary heat to fuse thick materials effectively at lower amperage settings. It is a workhorse for structural integrity in emergency situations.
The rod’s ability to maintain an arc even when the power supply fluctuates makes it a favorite for trail-side repairs. It produces a cleaner weld than typical 6011 rods, allowing for a better view of the puddle during the process. When the integrity of the weld must hold under heavy vibration, reach for the Fleetweld 180.
Blue Demon E6013: Best for Battery Welders
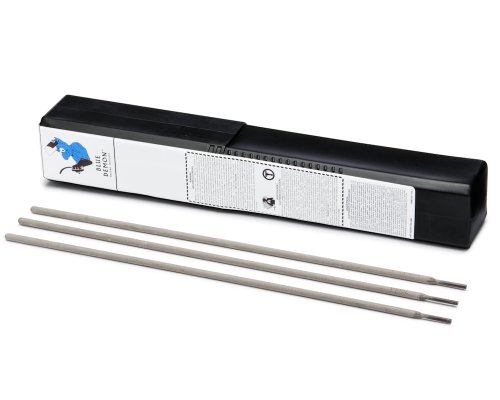
Battery-powered and ultra-portable welders often operate at lower open-circuit voltages than standard shop units. The Blue Demon E6013 is specifically formulated to strike easily and maintain a steady arc under these power-limited conditions. It is the go-to rod for small, lithium-ion battery welding setups common in backcountry overlanding.
This electrode is remarkably stable, which helps the welder maintain a consistent bead without the frequent arc-outs common to less-optimized rods. It is well-suited for smaller repairs where the operator lacks the constant, high-amperage power of a grid-tied machine. For the minimalist adventure traveler, the Blue Demon ensures the welder stays functional when it matters most.
ESAB Sureweld 7014: Best for Smooth Beads
Aesthetics matter for repairs that will remain visible, and the ESAB Sureweld 7014 provides a high-quality finish without demanding expert-level technique. This electrode features an iron powder coating that increases the deposition rate, resulting in a smooth, convex weld bead. It fills joints effectively with minimal effort from the welder.
Because it is easier to manage than deep-penetrating rods, it is perfect for finish work or when welding pieces that are already well-aligned. It produces very little slag, which reduces the time required for post-weld cleanup. For those who prioritize a clean, professional-looking repair on their gear, the 7014 is the clear winner.
Radnor E6010: Top Choice for Root Passes

The root pass—the first layer of a weld—is the most important part of a structural repair. The Radnor E6010 is known for its intense, digging arc that bites into the metal, making it the industry standard for securing the initial joint. In field repairs where pieces may have shifted, this rod pulls the materials together effectively.
It requires a practiced hand to control, as the arc is aggressive and unforgiving. However, for extreme conditions where total penetration is the only way to ensure the piece doesn’t fail again, the E6010 is essential. Pack a small supply of these for the most demanding, structural-critical repairs.
Matching Electrode Size to Trail Welders
The capacity of a portable welder dictates the electrode size, and pushing a machine beyond its duty cycle is a common mistake. Most portable field units operate best with 3/32-inch or 1/8-inch rods. Using a rod that is too thick for the machine results in an unstable arc and poor fusion.
- 3/32-inch electrodes: The universal choice for thin metal and battery-powered units.
- 1/8-inch electrodes: Best for structural, thick-wall steel repairs when the machine allows.
- Duty cycle awareness: Always check the welder’s rating; smaller rods draw less current, allowing for longer work sessions.
Always match the rod diameter to the output of the machine to ensure the welder stays within its design limits. Trying to “over-weld” with large rods on a small unit usually results in a blown fuse or a burnt-out circuit board, leaving the repair incomplete.
Prepping Dirty Metal for Emergency Repairs
Even the best electrode struggles when faced with excessive paint, thick rust, or heavy grease. A quick, aggressive scrub with a stainless steel wire brush is the minimum requirement for a successful repair. If the material is coated in thick rust, a small angle grinder or even a coarse metal file can save the rod from failing.
Removing the top layer of debris prevents gas porosity in the weld, which is what causes cracks to form later. While field conditions do not allow for a pristine surface, making an effort to expose bright, clean metal always leads to a stronger bond. Never skip the cleaning step, regardless of how urgent the repair feels.
Storing Electrodes to Keep Moisture Out
Welding rods are hygroscopic, meaning they absorb moisture from the air, which leads to poor performance and brittle welds. In the field, keep electrodes in a sealed, waterproof tube with a desiccant pack. This simple step preserves the chemical integrity of the flux coating throughout the life of the supply.
If rods are left exposed in a damp climate or high-humidity environment, the arc will become unstable and the slag will become difficult to remove. Store them inside the vehicle or inside a dry-bag when traversing wet terrain. Proper storage ensures the gear works correctly the moment it is needed.
Essential Safety Gear for Off-Grid Welding
Welding in the wilderness introduces unique safety challenges, including the risk of wildfire and eye damage. An auto-darkening welding helmet is non-negotiable, as it protects vision while allowing for precise placement in awkward positions. Additionally, high-quality, heat-resistant leather gloves protect against sparks and accidental burns.
Always carry a fire extinguisher or a heavy shovel for clearing dry debris before striking an arc. A welding apron or a heavy leather jacket prevents stray sparks from igniting synthetic hiking clothes or nylon gear. Safety is a component of the repair; an injury in a remote location is far more dangerous than a broken piece of equipment.
The ability to perform a field repair transforms a potential expedition-ender into nothing more than a minor delay. By selecting the right rod for the specific metal thickness and power supply available, the wilderness traveler gains a crucial layer of self-reliance. Carry a modest, well-maintained kit, practice the basics, and keep moving toward the next horizon.
Frequently Asked Questions (FAQs)
What is considered a low-amperage welding electrode?
A low-amperage welding electrode is a stick welding rod engineered to run effectively at settings below 90 amps, commonly between 40 and 80 amps. Small-diameter rods like 1/16-inch or 3/32-inch E6011 and E6013 allow welders to join thin sheet metals and light tubing without burning through the base steel. These electrodes produce a stable arc even when running on compact, low-output 120-volt inverter welders used on mobile job sites.
What does the flux coating do on low-amperage stick electrodes?
Flux coating on low-amperage stick electrodes vaporizes during welding to create a shielding gas envelope that protects the molten puddle from atmospheric contamination. Cellulosic coatings on rods like E6010 and E6011 provide a forceful, digging arc that burns through surface rust, oil, and mill scale. Rutile coatings on E6013 electrodes provide arc stabilizers that keep low-current arcs smooth and produce easily removable slag on light-gauge steel projects.
How do you set up low-amperage welding electrodes on a portable generator?
Setting up low-amperage welding electrodes on a portable generator requires matching the welder input wattage to clean generator power with less than 5% total harmonic distortion. Plug your inverter stick machine into a generator providing at least 3,000 to 5,000 continuous watts. Set the polarity to direct current electrode positive (DCEP) or alternating current (AC) depending on the rod classification, and dial the amperage knob between 50 and 70 amps for a 3/32-inch electrode.
How do you strike an arc with low-amperage welding electrodes without sticking?
Striking an arc with low-amperage electrodes works best using a match-scratch motion across the metal surface rather than tapping straight down. Drag the electrode tip lightly along the joint at a 15-degree angle until a spark catches, then immediately lift the tip about 1/8 inch to establish the arc length. Once the puddle stabilizes, tighten the arc gap to 1/16 inch to prevent voltage spikes that cause cold rods to fuse to the workpiece.
Which is better for low-amperage field use, 6011 or 7018 welding electrodes?
E6011 electrodes are generally better than standard E7018 electrodes for low-amperage field repairs because they tolerate dirty steel and operate cleanly on basic AC or DC power. An E6011 rod strikes easily at 50 amps and burns through outdoor paint and rust. In contrast, 7018 rods require moisture-controlled storage in rod ovens and frequently stick or produce porosity when run below 75 amps on portable machines, unless using specialized 7018 AC-rated variants.
How many pounds of low-amperage electrodes do you need for typical field repairs?
Most mobile field repairs require only a 5-pound or 10-pound tube of low-amperage electrodes to handle several days of maintenance tasks. A single 5-pound package contains roughly 80 to 90 individual 3/32-inch rods, which typically costs between $18 and $30 depending on the brand and alloy. Keeping sealed small tubes prevents moisture damage in mobile work trucks and avoids wasting money on bulk 50-pound cans that degrade in damp outdoor conditions.
Why is my low-amperage welding electrode sticking and extinguishing the arc?
Low-amperage welding electrodes stick and extinguish when the arc length is held too close or the machine amperage is set below the rod manufacturer threshold. Low-current arcs produce minimal heat and freeze instantly if the rod touches the puddle. Increase machine output by 5 to 10 amps, check that your work clamp has a clean bare-metal ground, and ensure your arc control or hot-start feature is engaged on your portable welder.
Can you safely run low-amperage welding electrodes on dirty or rusted outdoor metal?
Running low-amperage welding electrodes on rusted outdoor metal is structurally safe only if you use fast-freezing, high-penetration rods like E6010 or E6011. While these rods blast through light oxidation, severe grease and scale still cause internal slag inclusions and weld cracking. For heavy structural equipment, grind the repair zone down to shiny base metal before welding to guarantee proper weld fusion and operator safety.